Are your injection-moulded components developing unwanted edges, surface depressions, or incomplete sections? These defects can affect appearance, dimensional accuracy, functionality, and production costs.
Plastic injection moulding defects such as flash, sink marks, and short shots commonly result from unsuitable mould design, incorrect processing conditions, material behavior, or equipment problems.
Identifying the actual cause is essential before adjusting the machine or modifying the mould.
Parekh Wire Cut offers precision tooling and plastic injection mould manufacturing solutions for industrial applications.
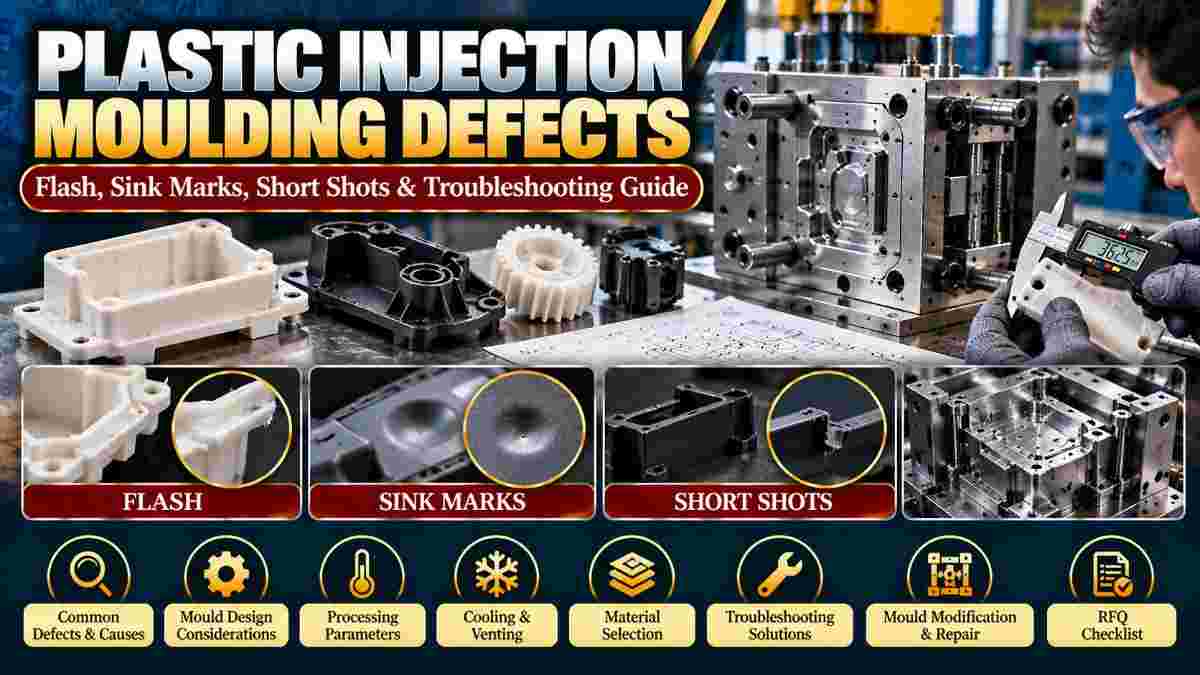
Common injection moulding defects include flash, sink marks, short shots, warpage, weld lines, burn marks, and surface imperfections.
Three particularly important defects are:
Flash: Unwanted plastic extending beyond the intended part boundary.
Sink marks: Localized depressions caused by uneven shrinkage.
Short shots: Incomplete filling of the mould cavity.
Each defect requires a different troubleshooting approach.
Flash occurs when molten plastic escapes through gaps at the mould parting line, inserts, ejector pins, or other sealing surfaces.
Common causes include:
Insufficient clamping force.
Excessive cavity pressure.
Damaged parting surfaces.
Poor mould alignment.
Worn tooling components.
Incorrect vent dimensions.
Flash may appear as thin plastic fins around the finished component.
Flash can be reduced by checking mould closure, clamping conditions, injection pressure, and the condition of sealing surfaces.
Recommended checks include:
Inspect the parting line.
Verify mould alignment.
Review clamping requirements.
Check injection and packing pressures.
Inspect shut-off surfaces.
Repair damaged tooling where necessary.
Avoid reducing pressure without checking whether the change causes incomplete filling or other defects.
Sink marks develop when internal material shrinkage pulls the outer surface inward during cooling, particularly around thick sections, ribs, and bosses.
Common causes include:
Uneven wall thickness.
Thick material sections.
Insufficient packing pressure.
Premature gate freezing.
Inadequate packing time.
Uneven cooling.
Unsuitable gate placement.
These defects often appear as shallow depressions on otherwise smooth surfaces.
Sink marks can be reduced by improving part geometry, packing conditions, cooling uniformity, and gate design.
Potential improvements include:
Maintaining suitable wall thickness.
Reducing excessive rib or boss thickness.
Optimizing packing pressure.
Reviewing packing time.
Improving cooling arrangements.
Evaluating gate size and location.
The correct solution depends on the material, part design, and moulding conditions.
A short shot occurs when molten plastic fails to completely fill the mould cavity before the material stops flowing or solidifies.
Possible causes include:
Insufficient injection pressure.
Low melt temperature.
Restricted gates or runners.
Poor venting.
Long flow paths.
Thin wall sections.
Inadequate shot volume.
Short shots may appear as missing corners, incomplete edges, or partially formed features.
Short shots can be reduced by checking melt flow, injection conditions, cavity venting, and mould geometry.
Troubleshooting may include:
Verify shot volume.
Check material temperature.
Review injection speed and pressure.
Inspect gates and runners.
Identify trapped air.
Evaluate thin sections.
Confirm machine capability.
Any process adjustment should remain within the material supplier's recommended processing limits.
Mould design influences how plastic enters, fills, packs, cools, and exits the cavity.
Important design elements include:
Runner layout.
Gate location.
Venting.
Cooling channels.
Cavity dimensions.
Parting surfaces.
Ejector arrangement.
Wall thickness.
Poorly designed features can make consistent production difficult even when machine settings are optimized.
Explore Plastic Injection Moulds for related tooling information.
Gate design controls material entry into the cavity, while venting allows displaced air and gases to escape during filling.
An unsuitable gate may contribute to restricted flow, uneven packing, or premature solidification.
Inadequate venting can cause short shots, trapped air, and surface defects.
Both features should be evaluated during mould design and troubleshooting.
Cooling affects shrinkage, dimensional stability, cycle time, and the likelihood of certain surface defects.
Uneven cooling can contribute to:
Sink marks.
Warpage.
Dimensional variations.
Residual stresses.
Inconsistent part appearance.
Cooling-channel placement and processing conditions should be evaluated together.
Mould modification may be necessary when defects persist after appropriate material, machine, and process checks.
Potential modifications include:
Repairing damaged shut-off surfaces.
Improving venting.
Adjusting gate geometry.
Modifying cooling channels.
Correcting cavity dimensions.
Reworking worn inserts.
Changes should be based on a documented root-cause investigation.
Precision CNC machining and Wire EDM can support the manufacture or correction of selected mould inserts, profiles, and tooling features.
Depending on the component, these processes may assist with:
Replacement inserts.
Precision profiles.
Tooling modifications.
Die components.
Dimensional corrections.
Explore CNC Wirecut EDM Services for related machining capabilities.
The appropriate repair method depends on the mould material, geometry, and approved drawing.
Buyers should provide complete product drawings, polymer specifications, production requirements, and quality expectations before ordering a mould.
An RFQ checklist should include:
Product 2D and 3D drawings.
Plastic material grade.
Finished part dimensions.
Critical tolerances.
Expected production volume.
Preferred cavity count.
Surface finish requirements.
Injection machine specifications.
Gate and appearance restrictions.
Inspection requirements.
Trial sample expectations.
Delivery requirements.
Accurate specifications help tooling manufacturers evaluate design feasibility.
Parekh Wire Cut provides plastic injection mould tooling and precision machining services for industrial manufacturing requirements.
Its website describes mould components, cavity design, cooling arrangements, and CNC machining capabilities.
Explore Plastic Injection Moulds for product information.
Confirm tooling specifications, inspection requirements, production capabilities, and commercial terms before ordering.
Common questions concern defect causes, machine settings, mould modifications, and quality improvement.
Yes. Excessive cavity pressure can contribute to flash, especially when mould sealing or clamping is inadequate.
Yes. Uneven cooling and shrinkage can contribute to sink marks, particularly around thicker sections.
Yes. Trapped air can prevent molten plastic from completely filling the cavity.
No. Some defects require changes to part geometry, tooling condition, gating, or cooling design.
Yes. Wire EDM can machine suitable electrically conductive mould components and precision tooling features.
You can request injection mould tooling services by sharing component drawings, plastic material details, defect photographs, production requirements, and inspection specifications.
For existing mould problems, include the observed defect locations and current processing information.
Explore Plastic Injection Moulds or visit Parekh Wire Cut to discuss your tooling requirements and request a quotation.
Technical Note: Injection moulding defects should be diagnosed through systematic process checks, material evaluation, tooling inspection, and approved engineering analysis before implementing corrective changes.